Features
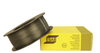
Dual Shield 9000-C1 is an all-position flux cored electrode which produces a 2.5% Ni deposit. The analysis is very similar to the Dual Shield T-90C1 except that this product has out-of-position capability. Dual Shield 9000-C1 is used for welding of 2-3% Ni steels and castings used in applications requiring good toughness at subzero temperatures. Shielding gas 100% CO2 and 75% Ar - Remainder CO2 may be used.
Industries
Process
Ship and Offshore Yards
Welding Process
Welding-FCAW - Flux Core Arc Welding
ESAB Welding and Cutting Products
Done
Description
Features
Dual Shield 9000-C1 is an all-position flux cored electrode which produces a 2.5% Ni deposit. The analysis is very similar to the Dual Shield T-90C1 except that this product has out-of-position capability. Dual Shield 9000-C1 is used for welding of 2-3% Ni steels and castings used in applications requiring good toughness at subzero temperatures. Shielding gas 100% CO2 and 75% Ar - Remainder CO2 may be used.
Industries
Process
Ship and Offshore Yards
Welding Process
Welding-FCAW - Flux Core Arc Welding
Features
Dual Shield 9000-C1 is an all-position flux cored electrode which produces a 2.5% Ni deposit. The analysis is very similar to the Dual Shield T-90C1 except that this product has out-of-position capability. Dual Shield 9000-C1 is used for welding of 2-3% Ni steels and castings used in applications requiring good toughness at subzero temperatures. Shielding gas 100% CO2 and 75% Ar - Remainder CO2 may be used.